What Is Fiber Laser Cutting?
Beyond "a laser cuts metal." Here's how a beam of near-infrared light is made inside a glass fiber, focused to a spot about the width of a human hair, and used with high-pressure gas to cut steel, stainless and aluminum — and what each step means for the parts you order.
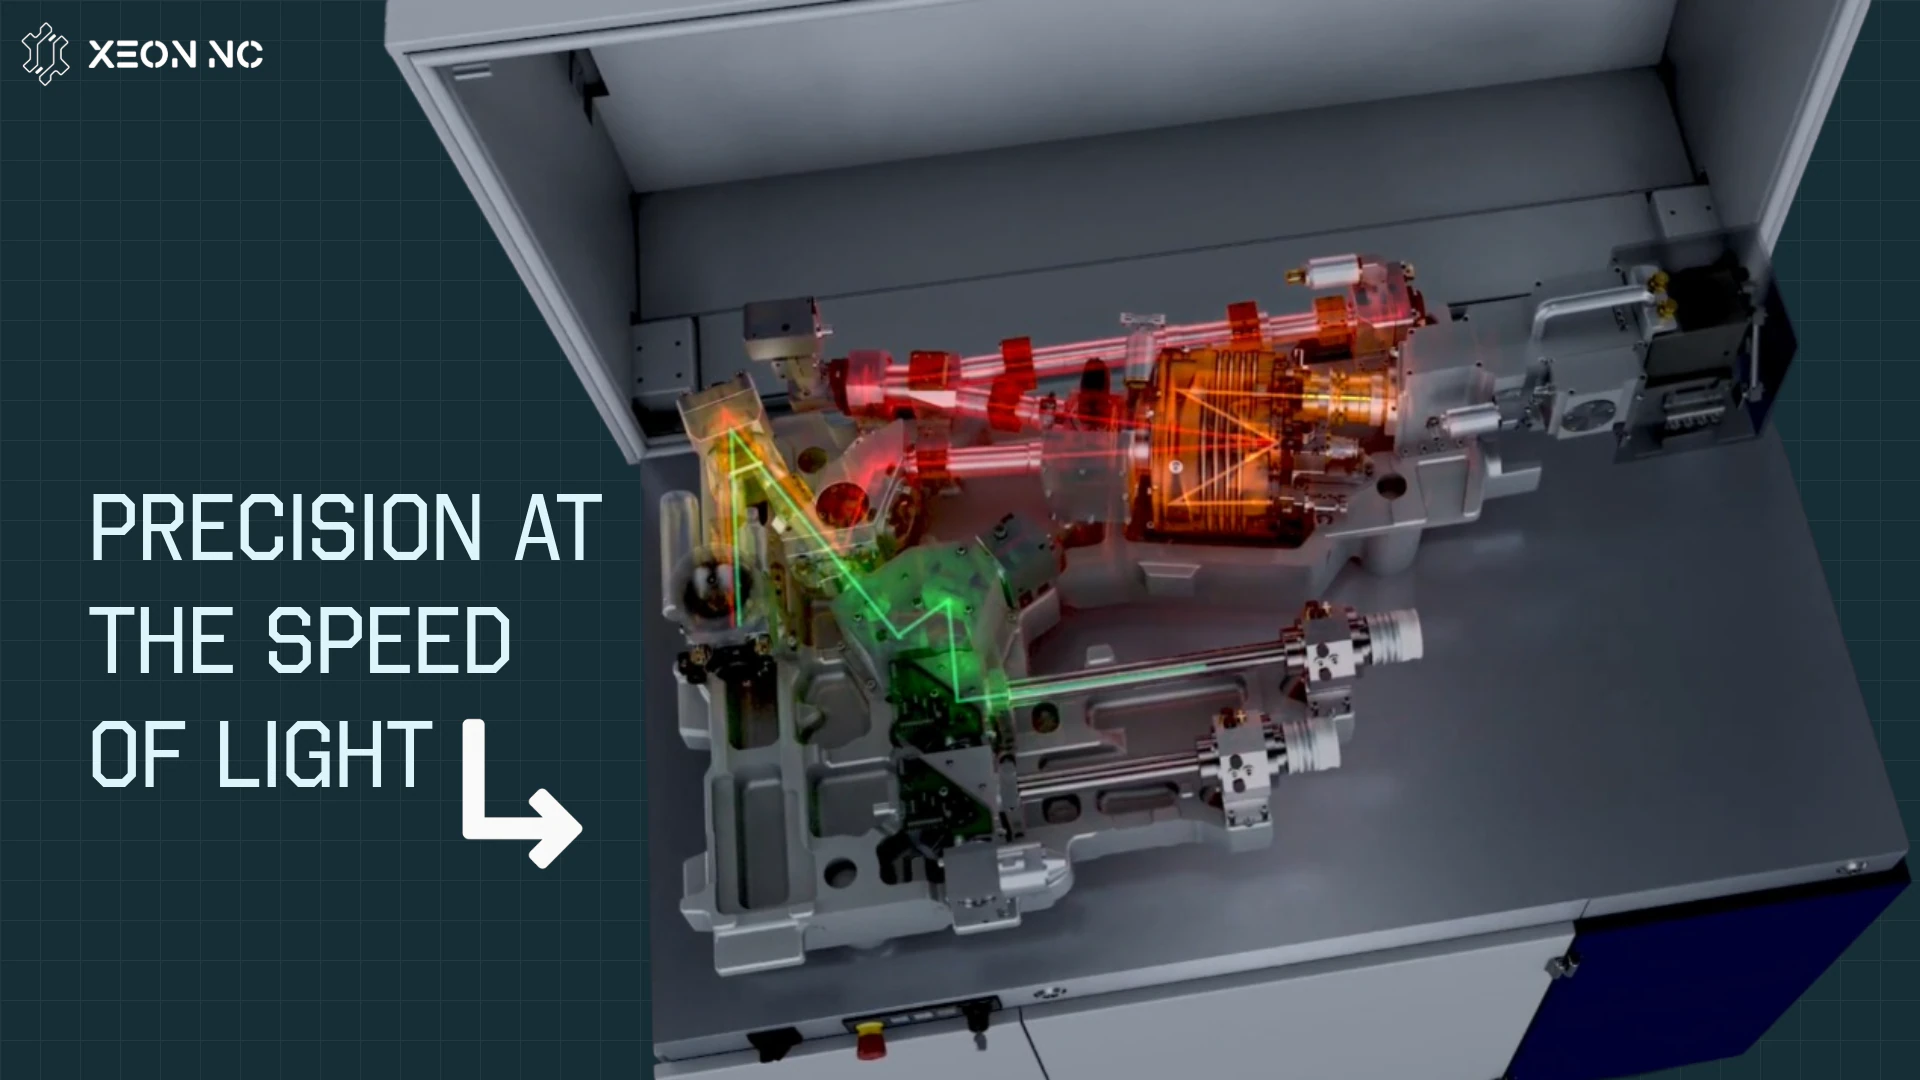
A fiber laser cutter doesn't really "burn" metal the way a torch does. It concentrates an enormous amount of light energy onto a microscopic point — so much that the metal there instantly melts or vaporizes — then blows the liquid away with a jet of gas, moving that point along your part's outline.
The word "fiber" describes where the light comes from: the laser beam is generated and amplified inside a doped optical fiber rather than a tube of gas or a slab of crystal. That one design choice gives fiber lasers their signature combination of efficiency, beam quality, reliability, and raw cutting speed. To really understand the process, it helps to follow the light from where it's created all the way down to the kerf it leaves behind.
Generating the Beam: Light Born in Glass
The heart of the machine is the fiber laser source. Instead of mirrors bouncing through a gas, the "active medium" is a long, thin optical fiber whose glass core is doped with a rare-earth element — usually ytterbium (Yb).
- Pump diodes — banks of semiconductor laser diodes pour light into the fiber, exciting the ytterbium atoms to a higher energy state.
- Stimulated emission — as those atoms relax, they release photons all at the same wavelength and phase, amplifying as they travel down the fiber. This is the "laser" effect (Light Amplification by Stimulated Emission of Radiation).
- ~1.06–1.07 µm wavelength — the resulting beam sits in the near-infrared. That short wavelength is absorbed far better by metals than older technologies, which is the whole game for cutting.
- Exceptional beam quality — because the light is confined inside a tiny fiber core, the beam is naturally clean and tightly focusable.
From Source to Sheet: The Beam's Journey
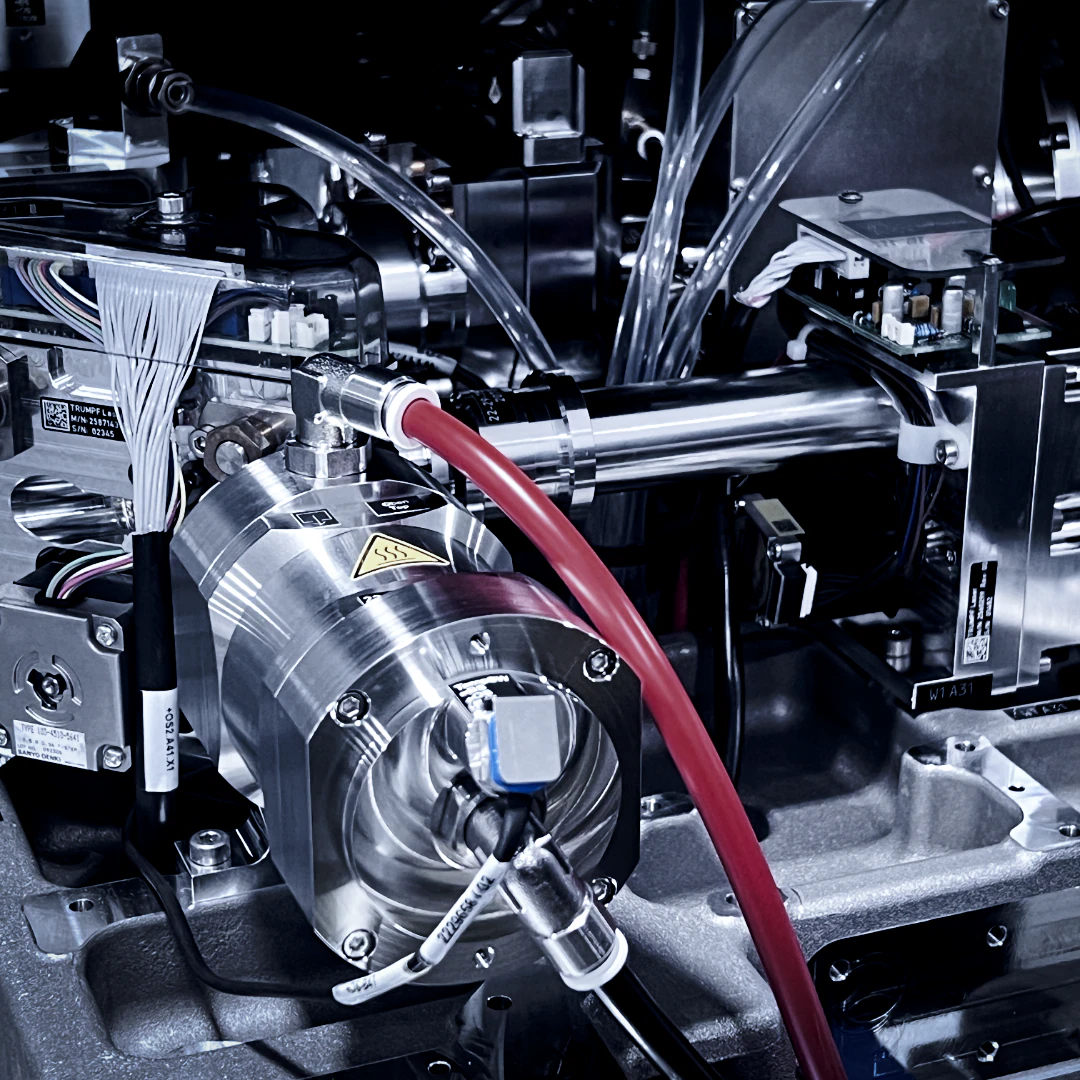
Once the beam exists, it has to travel from the source to the surface of your material and arrive as a focused, perfectly aligned point of light. In a fiber laser there are no delicate flying mirrors — the beam rides inside a flexible fiber-optic cable, then through a compact cutting head.
The numbers in the drawing match the steps below.
-
Transport fiberThe raw beam travels from the source through an armored fiber-optic cable to the cutting head — loss-free and immune to the misalignment that plagues mirror-based systems.
-
CollimatorThe beam exits the fiber diverging, so a collimating lens straightens it into a parallel column of light before focusing.
-
Focusing lensA focusing lens drives that column down to a tiny waist — a spot often just
~100–300 µmacross. This is where the energy density becomes extreme. -
Nozzle & assist gasThe focused beam exits through a nozzle that also delivers high-pressure assist gas coaxially with the beam, right at the cut zone.
-
Capacitive height controlThe head continuously senses and holds its standoff from the sheet, keeping the focus exactly where it needs to be even over warped or moving material.
How the Beam Actually Cuts Metal
Everything up to now exists to create one thing: an almost unimaginable concentration of energy on a single point. When that focused spot lands on metal, the physics happen fast.
Spot Size
at the Spot
Thin to Thick Sheet
- Absorption & heating — the metal absorbs the concentrated light and its temperature spikes past melting point in microseconds.
- Melt & vaporize — a tiny pool of molten (and partly vaporized) metal forms exactly at the focal point, no wider than the beam.
- Melt ejection — the coaxial assist gas blasts that molten material straight down and out the bottom of the cut, clearing the way.
- Motion makes the cut — the head traces your contour, and the continuous melt-and-eject leaves behind a clean, narrow kerf in the exact shape of your part.
Pierce and lead-in
Every cut starts with a pierce: the beam drills straight through the sheet before the head starts moving. Piercing leaves a small pit, and on thick plate it throws spatter, so the pierce goes in the scrap and a short lead-in carries the cut onto your part's edge. Thicker material needs a longer, more controlled pierce.
When there's no room for a lead-in — a very small hole, for example — the pierce lands close to the contour and can leave a small mark.
Assist Gas: Nitrogen, Shop Air & Oxygen
The assist gas isn't just there to clear debris — the gas you choose fundamentally changes the cut. Three options cover almost everything: nitrogen, oxygen, and plain shop air — and they cut by different mechanisms at very different costs.
- Inert — it doesn't react with the metal
- Purely blows molten material out of the kerf
- Leaves a clean, bright, oxide-free edge
- Ideal for stainless & aluminum that will be welded, coated, or left cosmetic
- Highest gas cost — typically 10–20+ bar at high flow
- Just clean, dry compressed air — ~78% N₂, 21% O₂
- By far the lowest-cost assist gas — no cylinders or bulk tank, only the compressor
- The nitrogen content blows a clean melt while the oxygen adds a little energy
- For thin-to-medium gauge it typically cuts faster than oxygen
- Leaves a light oxide — between nitrogen and oxygen edges
- Needs very clean, dry, oil-free air; limited on thick plate
- Reacts exothermically with the metal — the burn adds energy
- That extra heat lets it cut thicker carbon steel than air can
- Leaves a heavier oxide layer on the cut edge
- Low pressure — a few bar or less; the burn does much of the work
- Best for heavy mild steel where edge oxide is acceptable
The Parameters That Matter
A great cut is a recipe. For every material and thickness, our machines run a tuned set of parameters — nudge any one and the edge quality, speed, or reliability changes.
| Setting | What it controls | When it's off |
|---|---|---|
| Laser power | How much energy reaches the cut | Too little won't cut through; too much wastes heat and widens the kerf |
| Cutting speed | How fast the head moves along the outline | Too fast leaves dross or doesn't cut through; too slow burns the edge |
| Focal position | Where the narrowest point of the beam sits in the sheet | Rough or tapered edge, dross on the bottom |
| Assist gas + pressure | Which gas, and how hard it blows the melt out | Dross, extra oxide, or a rough edge |
| Nozzle | The size and shape of the gas jet | Gas misses the kerf and the melt isn't cleared |
| Standoff | The gap between nozzle and sheet | Focus and gas both drift; the height sensor holds it steady |
| Pierce settings | How the beam first breaks through | Spatter, a large pit, or a failed start on thick plate |
Power and speed are tuned as a pair for every material and thickness, so no two thicknesses run quite the same recipe.
Where the focus goes
For oxygen cutting of mild steel, the focus sits at or near the top surface; the burning reaction carries the cut down through the sheet. For nitrogen cutting of stainless and aluminum, it sits deep in the sheet. That opens the kerf lower down, so the high-pressure gas can push the melt out of the bottom.
Reading a Cut Edge
A laser-cut edge records how the cut went. Fine vertical lines, called striations, are normal: they're traces of the melt being blown out as the beam moves. Speed shows up most clearly.
| What you see | Usual cause | What to expect |
|---|---|---|
| Fine, nearly straight lines | Normal melt flow | Finer on thin sheet, more visible on thick plate |
| Lines that sweep back near the bottom | Cutting too fast for the thickness | A recipe problem, fixed by slowing down |
| Beads on the bottom edge (dross) | Speed, focus or gas pressure off; more common on thick plate | Light dross comes off with deburring |
| Rough, dark or wide edge | Too slow, or heat building up in tight corners | The machine lowers power in corners to limit it |
| Small mark where the cut starts | The pierce or lead-in | Placed in the scrap wherever the part allows |
Why Fiber Beat CO₂
For decades, CO₂ lasers dominated metal cutting. Fiber lasers have largely displaced them for sheet metal — and the reasons are concrete, not marketing.
| Attribute | Fiber Laser | CO₂ Laser |
|---|---|---|
| Wavelength | ~1.06 µm (near-IR) | 10.6 µm (far-IR) |
| Beam delivery | Flexible fiber cable | Mirrors & alignment |
| Wall-plug efficiency | ~30–40% | ~10% |
| Thin-sheet speed | Significantly faster | Slower |
| Reflective metals | Cuts Al, Cu, brass well | Struggles / risky |
| Maintenance | No laser gas, no mirrors | Mirrors, gas, more upkeep |
| Very thick plate | Cuts it; the edge can be rougher | Often a smoother edge |
The short version: fiber lasers turn more electricity into usable light, deliver it without fragile optics, cut thin and reflective material faster, and need far less maintenance. CO₂ can still leave a smoother edge on very thick plate, but for sheet metal fiber wins. That's why our floor runs fiber.
What It Means for Your Parts
All of this physics shows up in the part you receive. Four things are worth understanding as a designer:
- Kerf — the beam removes a narrow strip, about 0.006–0.014″ wide depending on thickness. The software offsets the beam path by half the kerf, so your dimensions land on target. More in the laser kerf guide and the kerf rule of our design guide.
- Heat-affected zone (HAZ) — a thin band beside the cut sees brief intense heat. Fiber's fast, focused cut keeps it small; the HAZ guide covers how it affects the material.
- Taper and dross — the kerf is slightly wider at the top, and thick plate can leave a small bead on the bottom edge. See Reading a Cut Edge above.
- Edge quality and tolerances — clean, square, repeatable edges across a full sheet, typically ±0.005″ on cut features. To design parts that get the most from the process, read our laser cutting design guide.