Our Press Brake Tooling Library
Every punch and V-die we run on the Xeon NC press brake, the material thickness each die covers under the 6–12 die-width rule, and the full technical data for each WILA OW / EV tool — so you know your part can be formed before it is ever quoted.
Form it before
you quote it.
The live inventory of our tool cabinet
and exactly which gauge each piece forms
Scroll to explore
The tool stack decides the bend.
Bend quality is decided by the tool stack, not the part. The V-die opening sets the radius, the tonnage, and the smallest flange you can form; the punch sets the angle you can reach and whether it clears the part on the way down. This page is the live inventory of what is physically in our tool cabinet — and exactly which gauge each piece is built to form.
The dies below are WILA / Trumpf-style EV bottom tools and the punches are OW top tools, all ground from 42CrMo4 tool steel and induction hardened to ~60 HRC. Match your material thickness to a die using the rule in the next section, then confirm the whole stack on our 2D Bend Check — it renders these exact tool profiles against your flat pattern. Dimensions show in inches by default; flip any toggle to switch the whole page to millimetres.
The 6–12 die-width rule
Explore the coverage
The single rule that maps a die to a thickness: the V-die opening should be 6 to 12 times the material thickness. Thin or soft material sits at the low end of that range; thick or high-strength material needs the wide end to avoid cracking the outer fibre and to keep tonnage in check.
So every die owns a thickness band: from V ÷ 12 at the thin end to V ÷ 6 at the thick end. Run thinner than V ÷ 12 and the part over-bends into a sharp, unrepeatable radius; run thicker than V ÷ 6 and you risk outer-fibre cracking and over-tonnage.
Each bar is the band a die can form (V ÷ 12 → V ÷ 6). Hover a bar for its exact range. Together our five dies cover roughly 0.03″–0.33″ (0.7–8.3 mm) — 22 ga through 5⁄16″ plate.
- 1
Tight end, 6×. Aluminium tolerates it: a narrower V gives a tighter radius and a shorter minimum flange.
- 2
Wide end, 10–12×. Stainless and high-strength steel want it: a softer radius and lower tonnage.
- 3
Overlap is normal. The thin bars (EV002) run into the next die up — pick the narrower V for radius, the wider V for tonnage.
- 4
Rule of thumb, not a hard wall. When two dies overlap a thickness, the choice comes down to radius versus tonnage.
Inside the tool cabinet.
V-dies on the top row, punches below. Open any tool for its traced profile, material range and technical data.
 01 / V-dieEV002
≈ 22 – 16 gaView tool
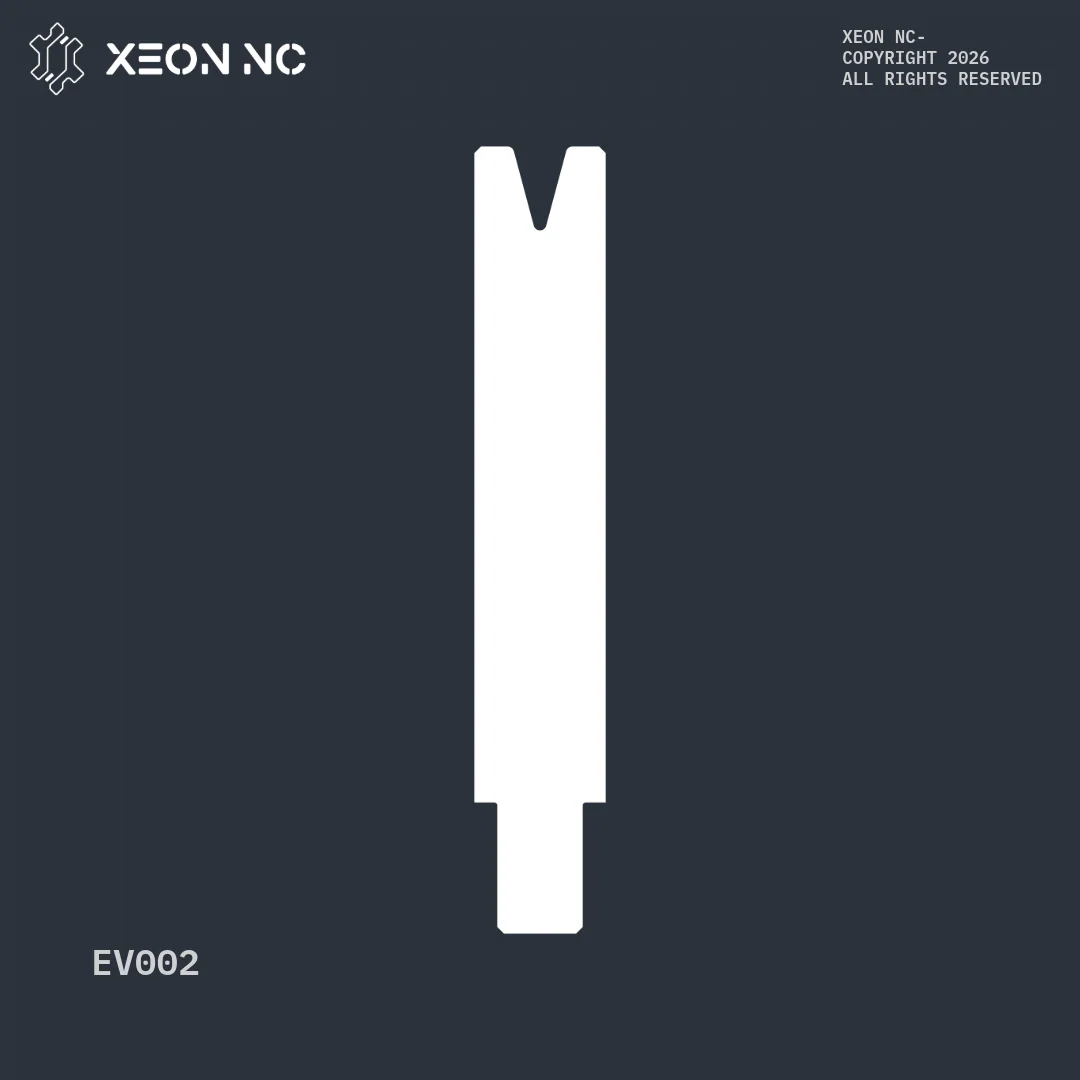
Lower · V-Die / W8 / 30° · R1
EV002
Our tightest die. Thin-gauge work and small inside radii.
Material range · ≈ 22 – 16 ga
 02 / V-dieEV004
≈ 19 – 14 gaView tool
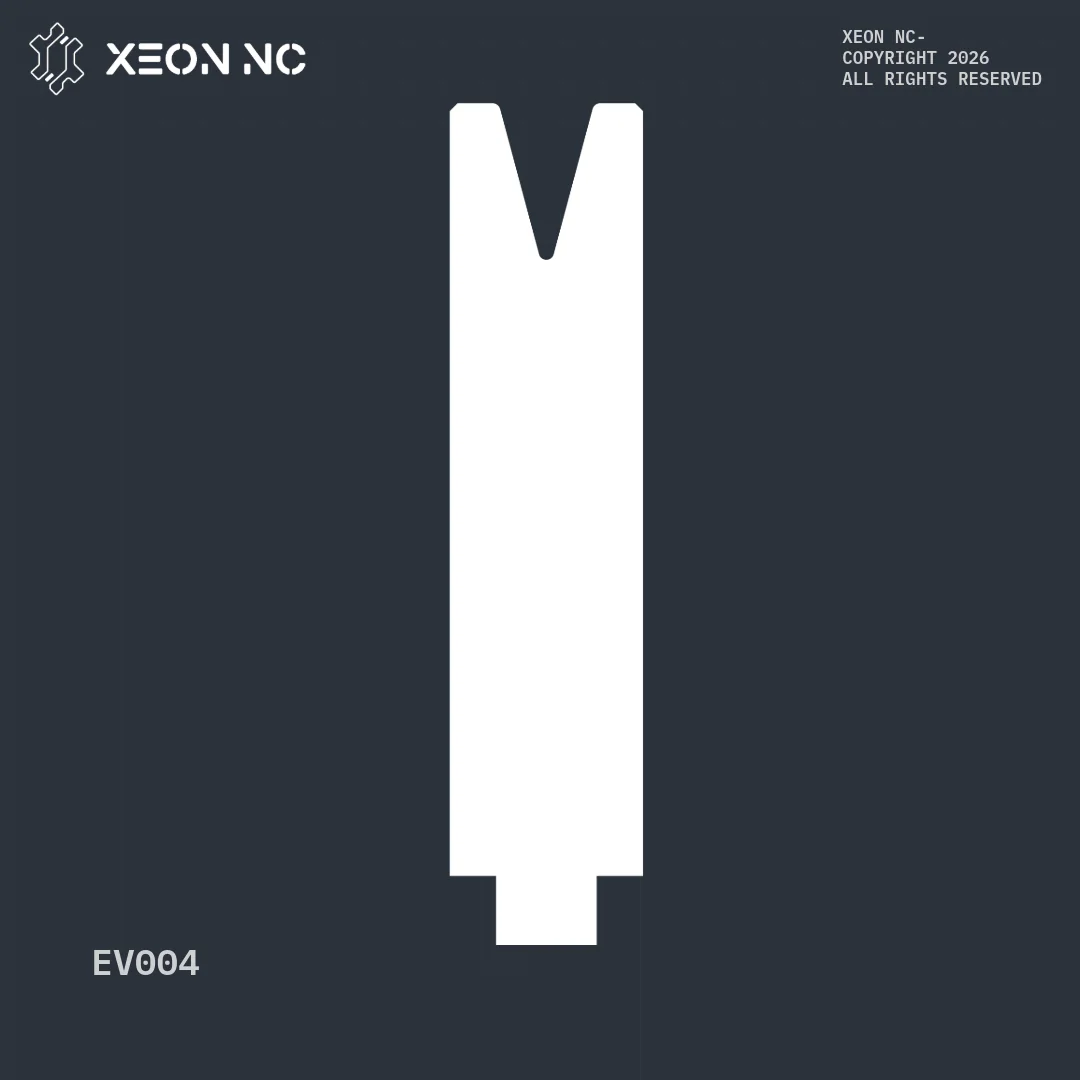
Lower · V-Die / W12 / 30° · R1
EV004
The everyday die for light sheet.
Material range · ≈ 19 – 14 ga
 03 / V-dieEV006
≈ 14 – 10 gaView tool
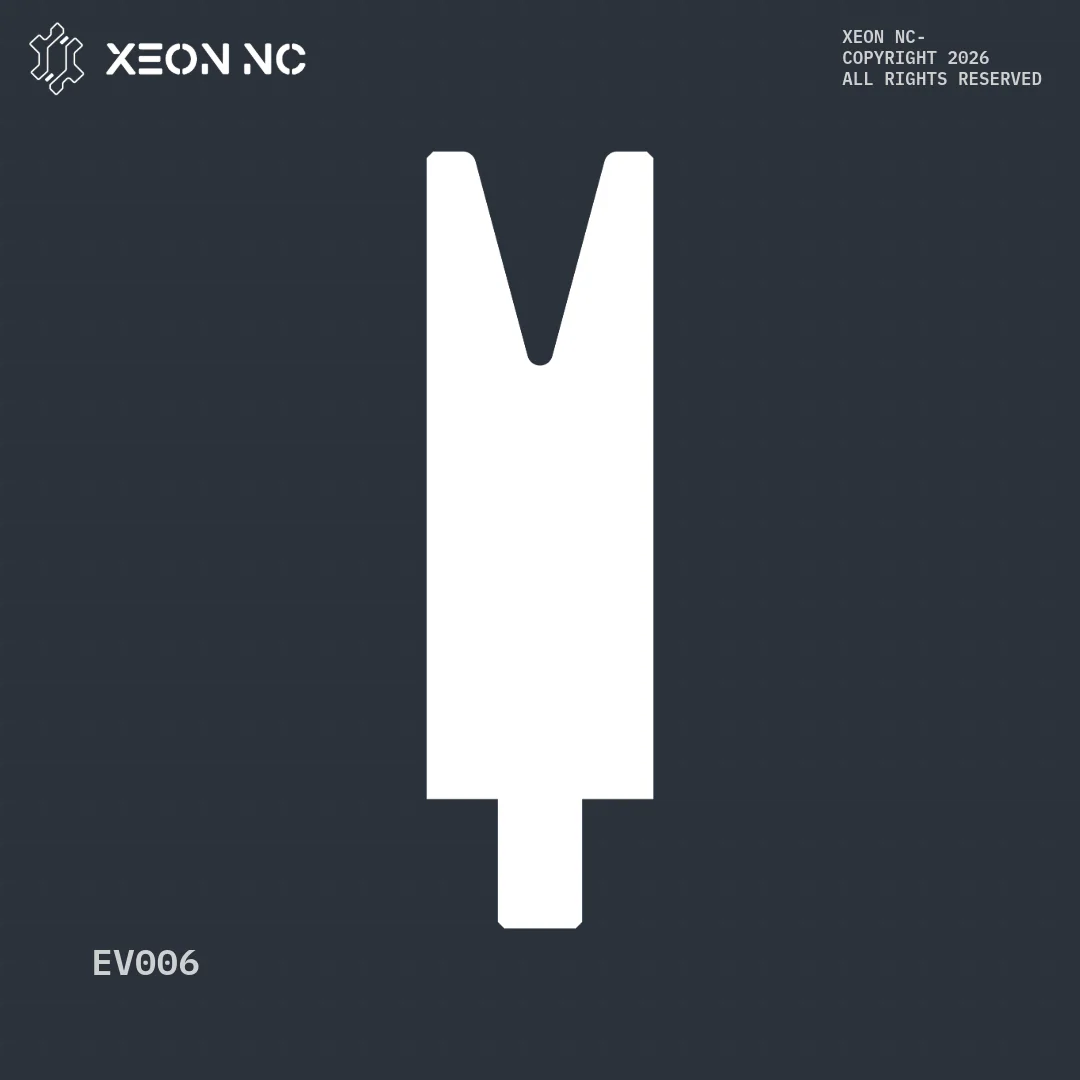
Lower · V-Die / W20 / 30° · R2
EV006
Mid-gauge die with a softer R2 floor.
Material range · ≈ 14 – 10 ga
 04 / V-dieEV W30/80
≈ 12 – 7 gaView tool
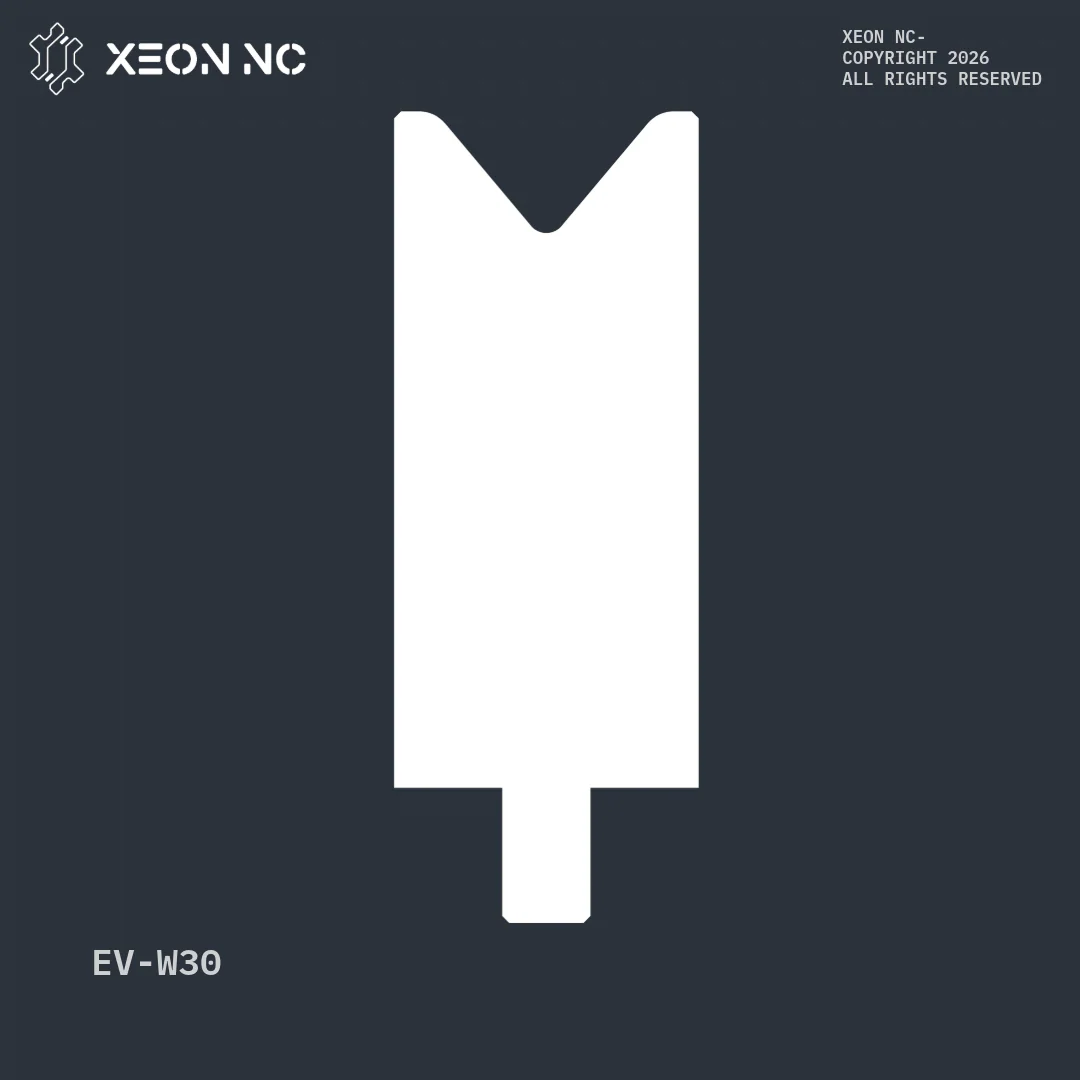
Lower · V-Die / W30 / 80° · R5
EV W30/80
Wide 80° die with a large R5 floor for heavy gauge and soft radii.
Material range · ≈ 12 – 7 ga
 05 / V-dieEV W50/80
≈ 8 ga – 5⁄16″View tool
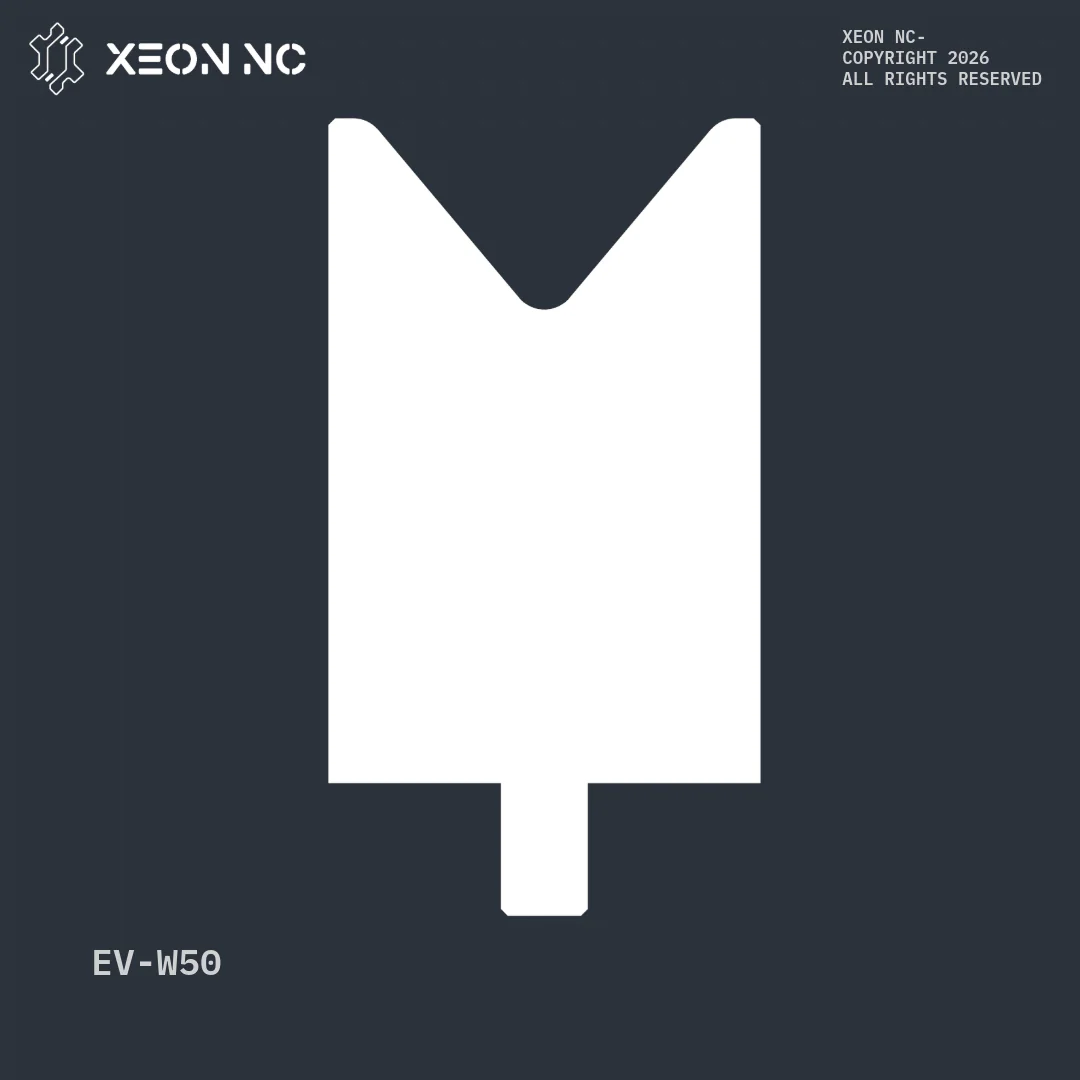
Lower · V-Die / W50 / 80° · R5
EV W50/80
Our widest die. Plate work, large radii, lowest tonnage per bend.
Material range · ≈ 8 ga – 5⁄16″
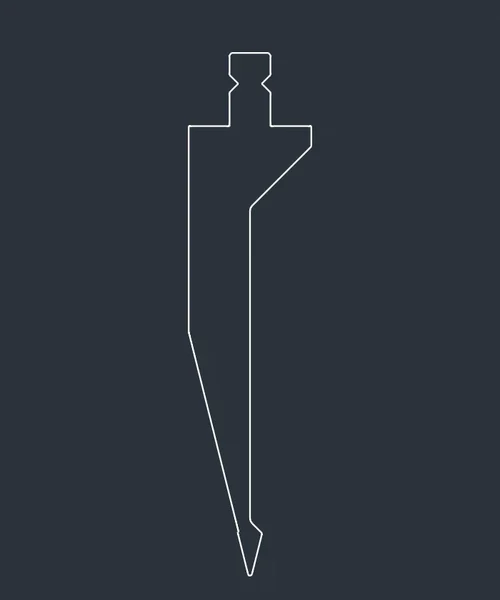 06 / PunchOW202/S
R1 / 28° · H220View tool
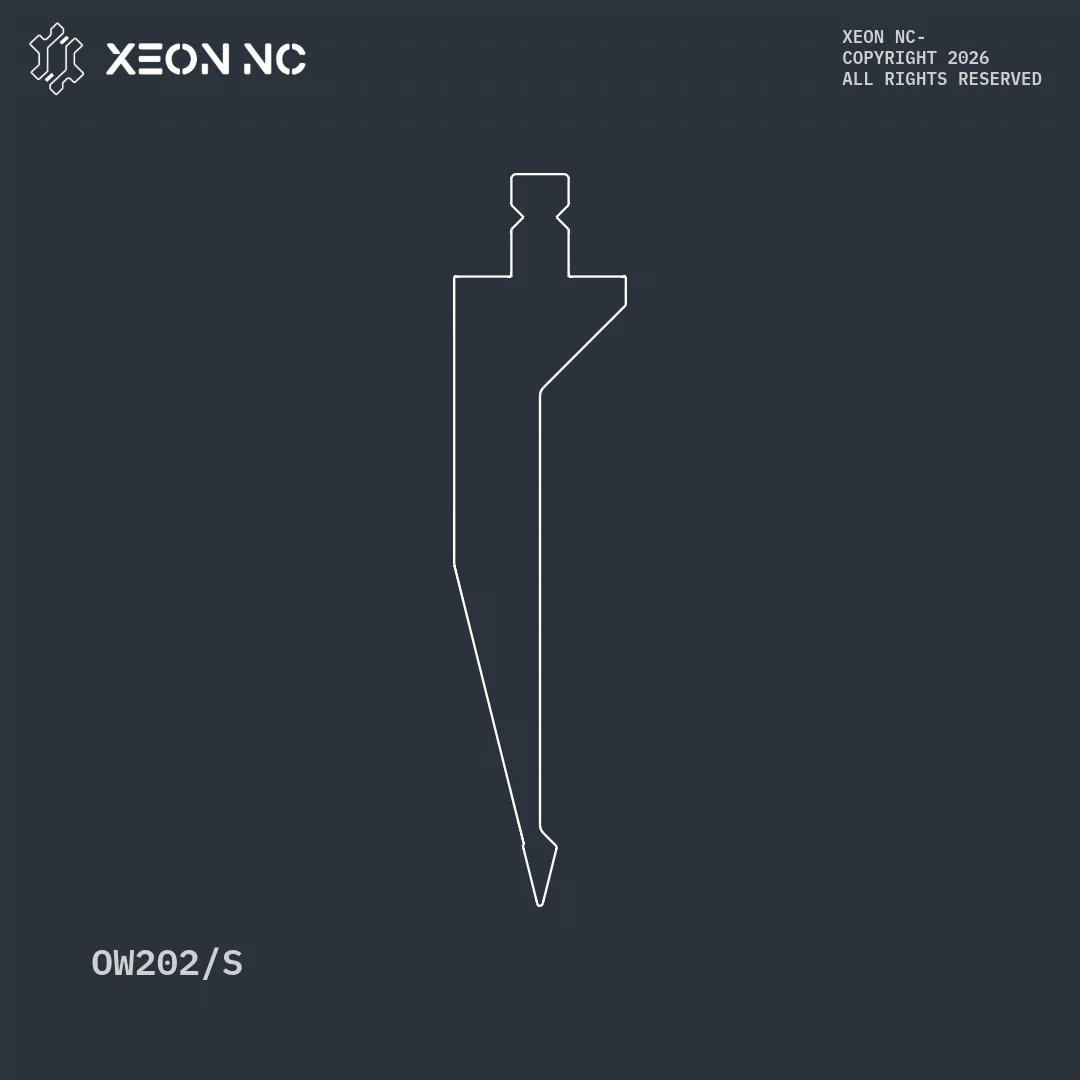
Upper · Punch / R1 / 28° · H220
OW202/S
Sharp 28° pointed punch, tall body. Acute and standard bends where flanges need clearance. Flippable.
07 / PunchOW202/K
R1 / 28° · H120View tool
Upper · Punch / R1 / 28° · H120
OW202/K
The short-body version of the OW202 sharp punch. Same 28° tip, lower stack height for shallow parts. Flippable.
 08 / PunchOW200/S
R1 / 86° · H220View tool
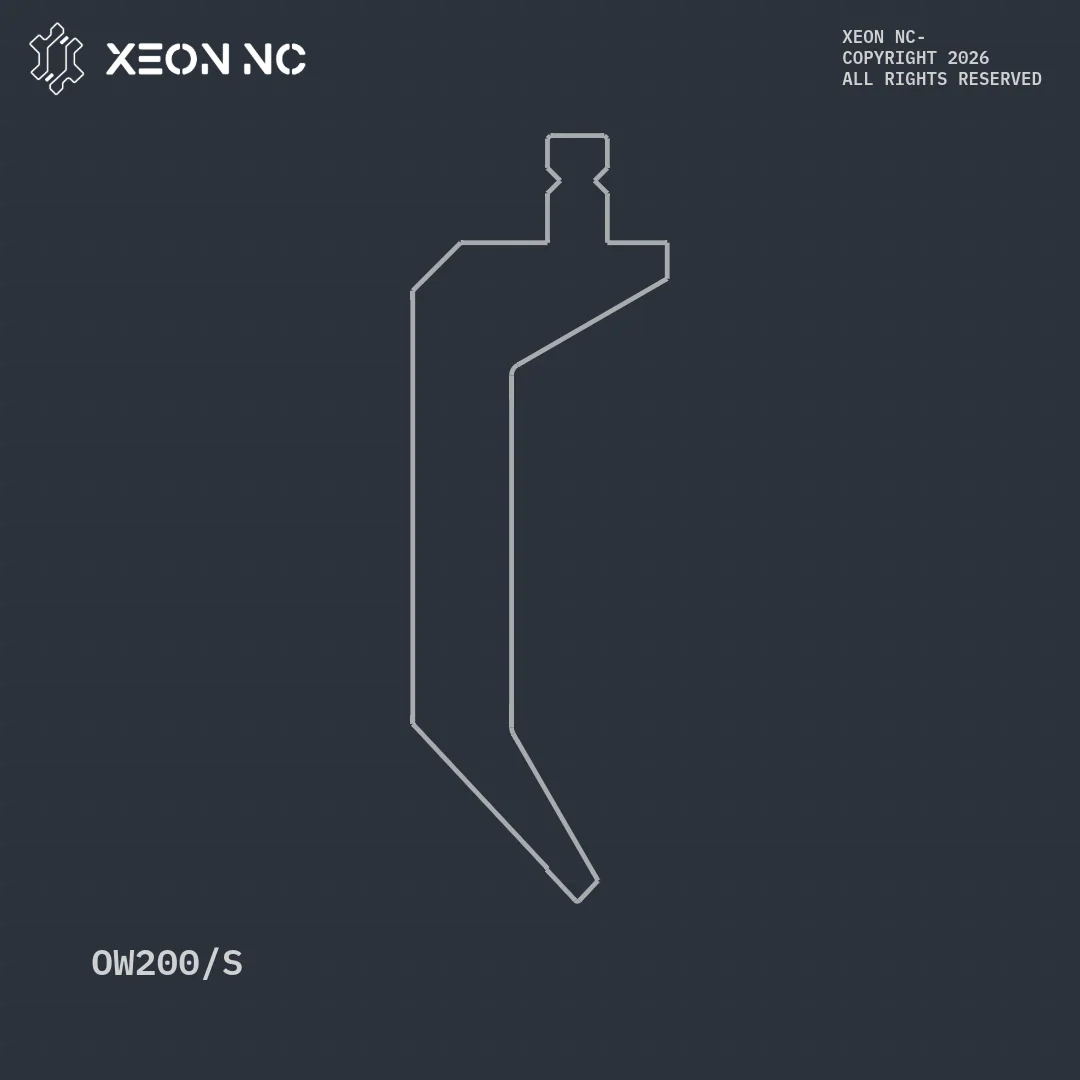
Upper · Punch / R1 / 86° · H220
OW200/S
Gooseneck punch. The curved relief reaches over a previously formed return flange. 86° for standard 90° work. Flippable.
 09 / PunchOW300/S
R1 / 86° · H300View tool
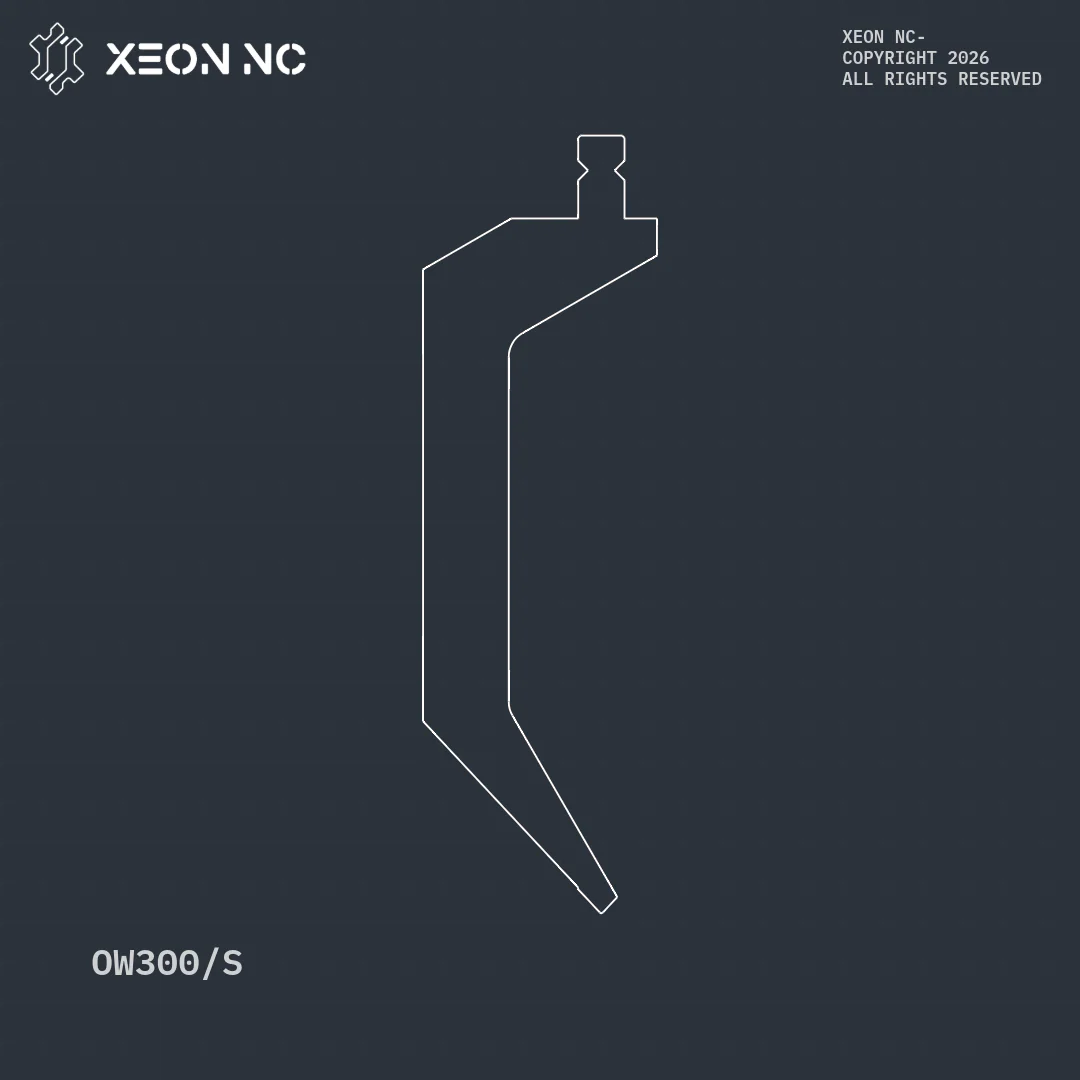
Upper · Punch / R1 / 86° · H300
OW300/S
Extra-tall gooseneck for deep boxes and pans. Clears tall opposing flanges a 220 mm tool would crash into. Flippable.
 10 / PunchOW203/S
R4 / 60° · H220View tool
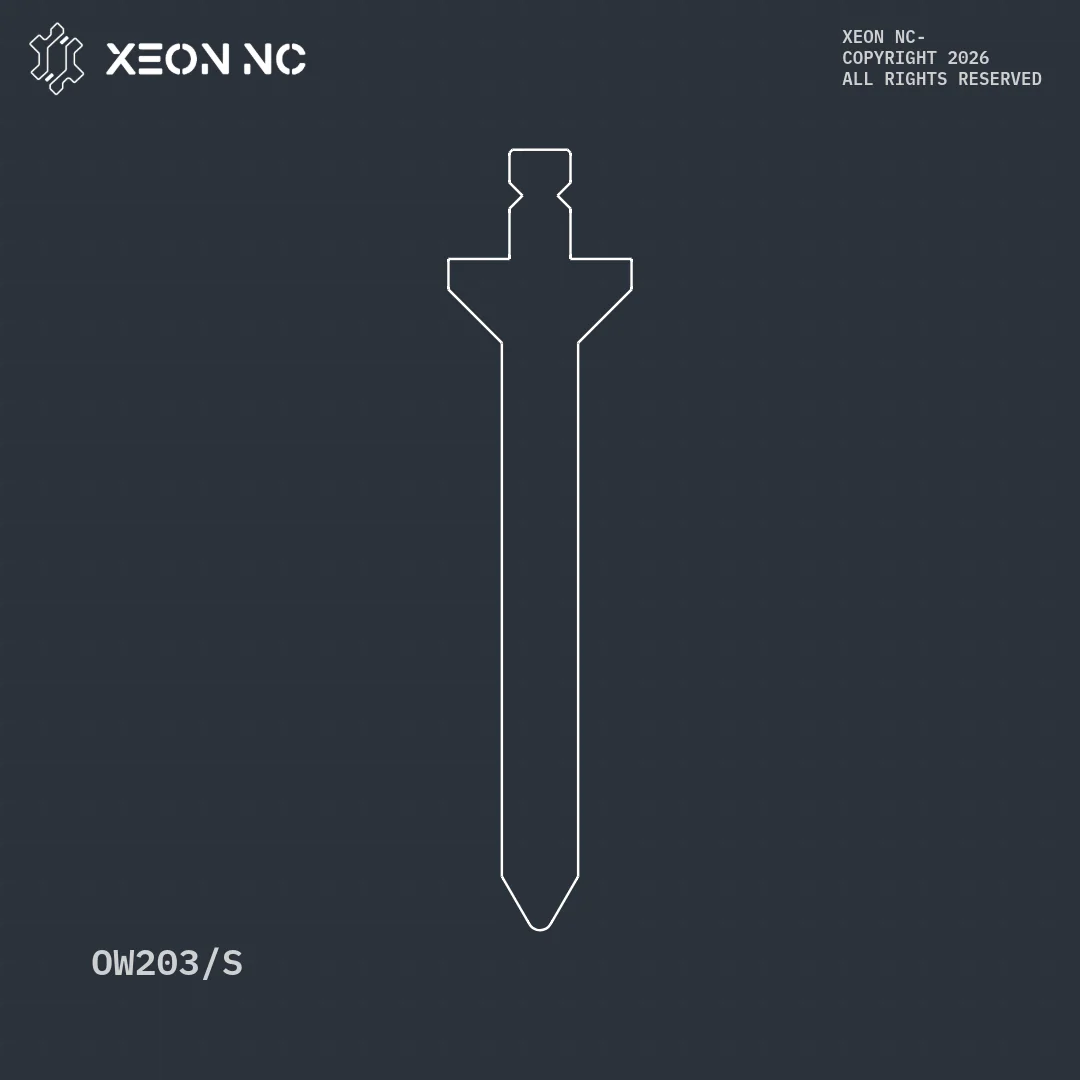
Upper · Punch / R4 / 60° · H220
OW203/S
Heavy straight punch with a large R4 tip. Soft inside radii and high-tonnage plate work. Highest rated load in the library.
Single-V air-bending dies, WILA / Trumpf EV style, seated in the standard DTrumpf lower clamp. The die opening sets the radius and the tonnage; the die angle (30° or 80°) sets how acute a bend it can clear.
OW top tools seated in the PTrumpf upper clamp. A punch is not chosen by thickness — it is chosen by three things: the tip radius (the smallest inside radius it can press), the included angle (how acute a bend it can reach), and the height (how tall an adjacent flange it can clear without colliding). Pair any of these with the die that matches your gauge.
V-opening, angle, tip radius, height and tonnage are read directly from each tool's CAD file and follow the page unit (inches by default). Which punch clears your part? The Reverse Bend Clearance Checker computes the max return flange height for every punch from these same traced profiles.
Five dies. Five punches. 22 gauge through 5⁄16″ plate.
V-dies — thickness coverage
| Die | V-opening | Angle | Radius | Thickness (6–12) | Gauge |
|---|---|---|---|---|---|
| EV002 | 30° | R1 | 22 – 16 ga | ||
| EV004 | 30° | R1 | 19 – 14 ga | ||
| EV006 | 30° | R2 | 14 – 10 ga | ||
| EV W30/80 | 80° | R5 | 12 – 7 ga | ||
| EV W50/80 | 80° | R5 | 8 ga – 5⁄16″ |
Punches — selection by geometry
| Punch | Tip R | Angle | Height | Type | Rated load |
|---|---|---|---|---|---|
| OW202/S | R1 | 28° | Pointed / acute | 600 t/m | |
| OW202/K | R1 | 28° | Pointed / acute | 600 t/m | |
| OW200/S | R1 | 86° | Gooseneck | 800 t/m | |
| OW300/S | R1 | 86° | Gooseneck | 800 t/m | |
| OW203/S | R4 | 60° | Straight / large-R | 2500 t/m |
Gauge equivalents & data sources
Geometry figures are read from each tool's CAD file. Gauge equivalents are nominal steel; aluminium and stainless shift the band toward the tight and wide ends of the 6–12 window respectively.
Need a spec that isn't listed?
Tool weights, load ratings, and mounting notes are on file in the shop. Email quote@xeonnc.com with the tool ID and we'll send the full data sheet.
Check your part against these exact tools
Open the Bend Simulator
The 2D Bend Check renders these punch and die profiles against your flat pattern — recommended V, predicted radius, tonnage, and collision warnings before you order.
Reverse Bend Clearance Checker
Enter a base dimension and flange height and see which of these punches reach the bend without colliding with the return flange.